

Thứ năm, 17/09/2026 | 09:35


ABSTRACT Ti-6Al-4V (Ti64) alloy is the most popular Titanium alloy used in the industry. However, it is described as a difficult-to-process material because of its poor tribological performance, which leads to a higher friction coefficient, severe adhesion, and significantly low thermal dissipation. In griding process, cubic boron nitride (cBN) grinding wheels are an industrially attractive and long-term stable tool selection for hard-to-machine metallic alloys, due to their high productivity, high cutting reliability, and low thermal damage. This research evaluates the machining characteristics of Ti64 through surface grinding experiments using a resinoid cBN grinding wheel with a grit size of #120. The effect of technology parameters including tangential feeding and depth of cut (DOC) to the surface roughness is presented. The results show that surface roughness is significantly affected by grinding parameters. The increase of feedrate or depth of cut both introduce higher surface roughness. The effect of DOCis more apparent than those of tangential feeding. The experimental results show that optimum feedrate of 3000mm/minwould produce theminimum surface roughness. Keywords: Titanium alloy, resinoid cBN grinding wheel, surface roughness, optimum cutting condition, surface grinding. |
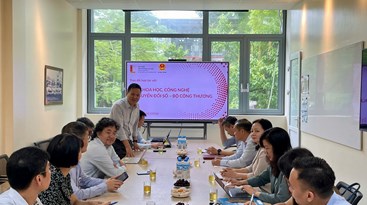
Sáng 16/9, tại Hà Nội, Cục Khoa học, Công nghệ và Chuyển đổi số, Bộ Công Thương có buổi làm việc với Đại học Bách khoa Hà Nội nhằm trao đổi về tiềm năng, định hướng hợp tác trong nghiên cứu khoa học, phát triển công nghệ, đổi mới sáng tạo và chuyển đổi số, gắn với yêu cầu phát triển các lĩnh vực công nghiệp, công nghệ chiến lược của ngành Công Thương.
16/09/2026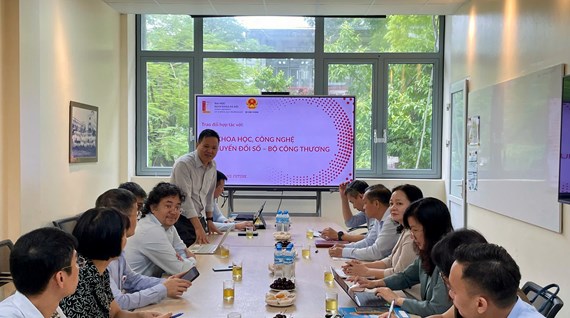
Sáng 16/9, tại Hà Nội, Cục Khoa học, Công nghệ và Chuyển đổi số, Bộ Công Thương có buổi làm việc với Đại học Bách khoa Hà Nội nhằm trao đổi về tiềm năng, định hướng hợp tác trong nghiên cứu khoa học, phát triển công nghệ, đổi mới sáng tạo và chuyển đổi số, gắn với yêu cầu phát triển các lĩnh vực công nghiệp, công nghệ chiến lược của ngành Công Thương.
16/09/2026